Product Category
Water ring, dry, and oil-sealed vacuum pumps for industrial vacuum applications across chemical and process industries.
Our Range
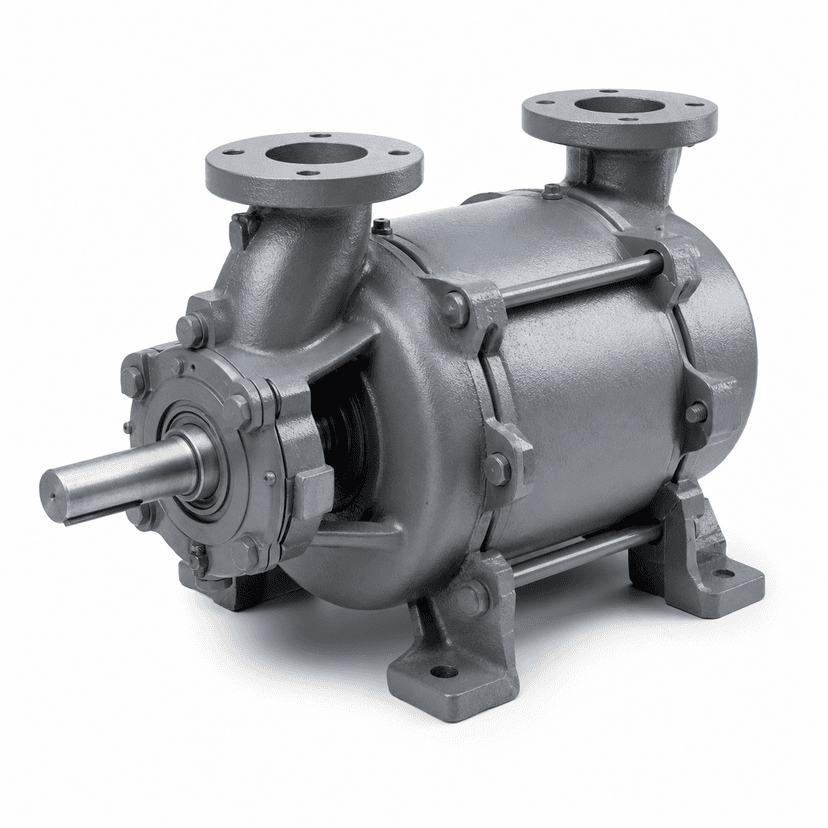
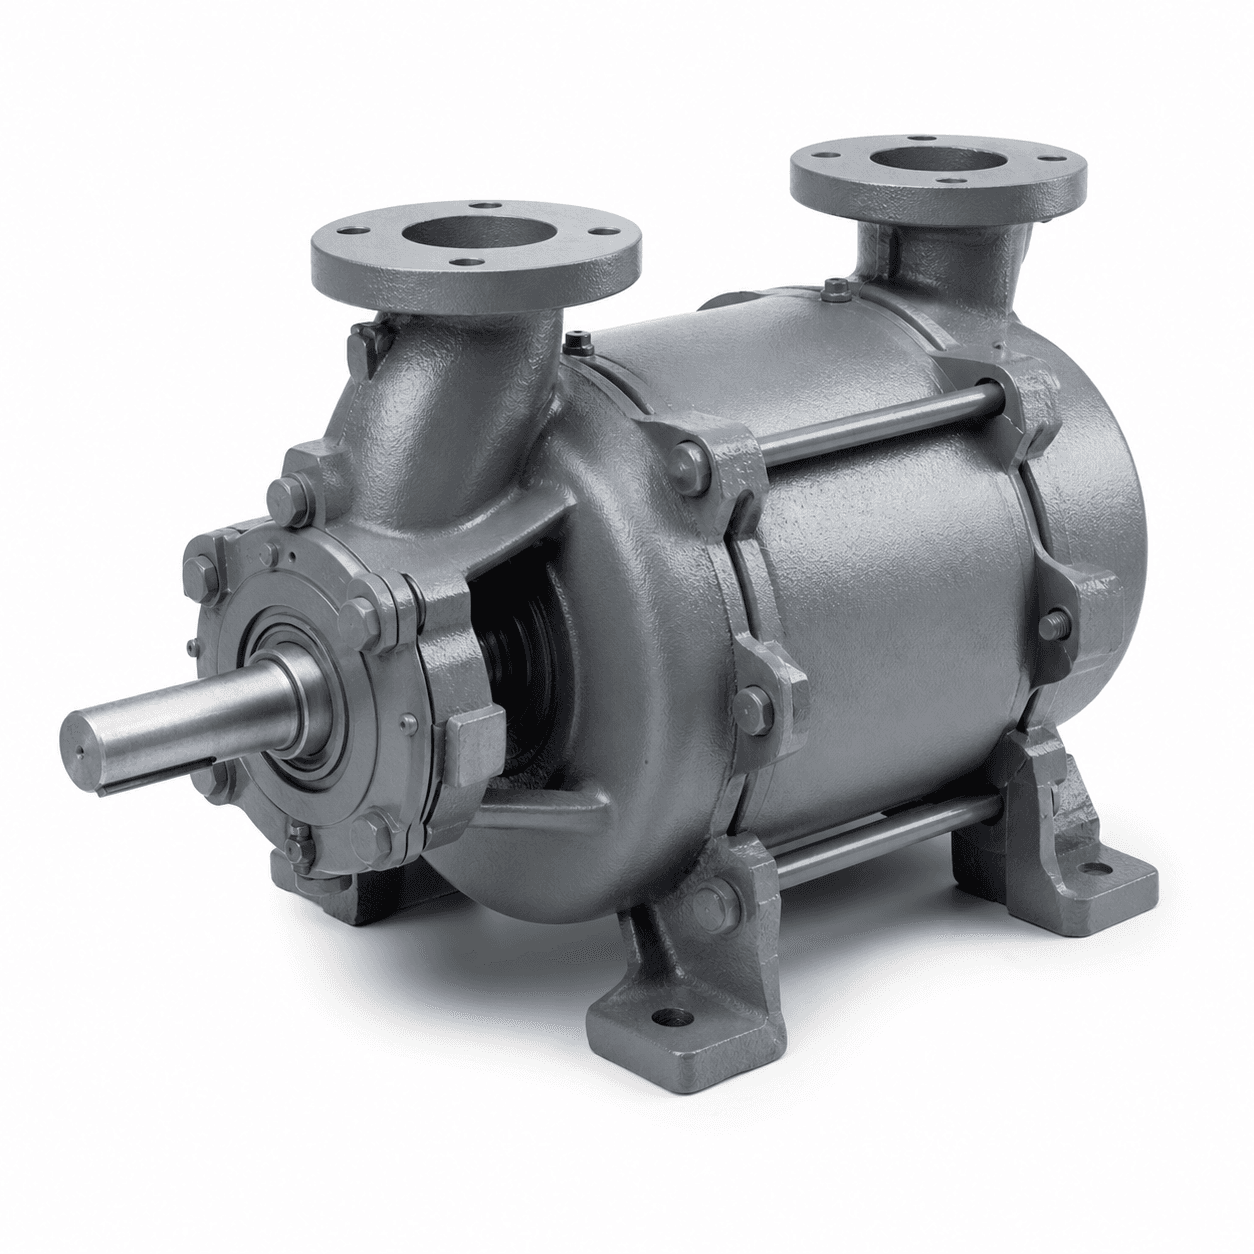
High-vacuum oil sealed rotary vane pump achieving up to 0.005 mbar. Oil sealed for deep vacuum with high efficiency and low noise operation.
Single stage water ring vacuum pump achieving up to 30 mbar. Uses water as sealing medium, safely handles moisture, steam, and wet vapors.
Double stage water ring vacuum pump achieving up to 10 mbar. Dual impellers provide deeper vacuum for wet gas applications in pharma and chemical industries.
Ultra-compact monoblock vacuum pump with motor and pump on a single shaft. No coupling required, easy setup, ideal for small plants and OEM integration.
FAQ
Common questions about this product category.
Oil sealed vacuum pumps achieve deeper vacuum (up to 0.005 mbar) using oil as the sealing medium, suited for clean, dry applications like packaging and labs. Water ring vacuum pumps use water as the seal (up to 30 mbar single stage, 10 mbar double stage) and safely handle moisture, steam, and wet vapors, suited for paper, textile, chemical, and pharma industries.
A monoblock vacuum pump has the motor and pump on a single shaft with no coupling, making it ultra-compact, easy to set up, and space-saving. It is ideal for small plants, OEM integration, and liquid or vapor extraction applications where space is limited.
Explore More
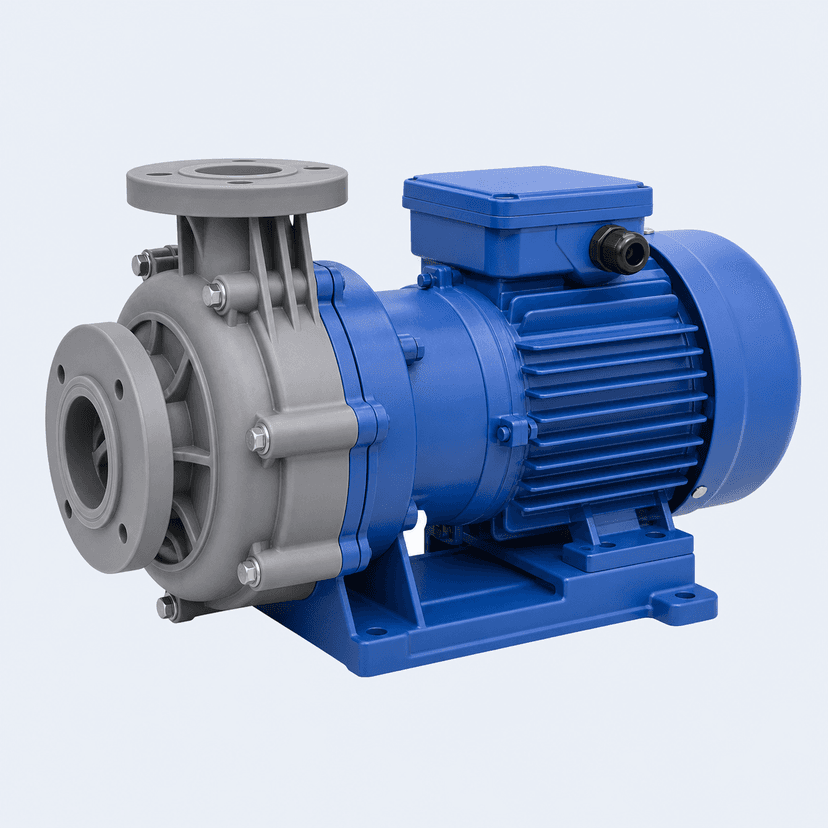
Horizontal centrifugal pumps with corrosion-resistant PP, PVDF, GRP, and UHMWPE construction for chemical and process industries.
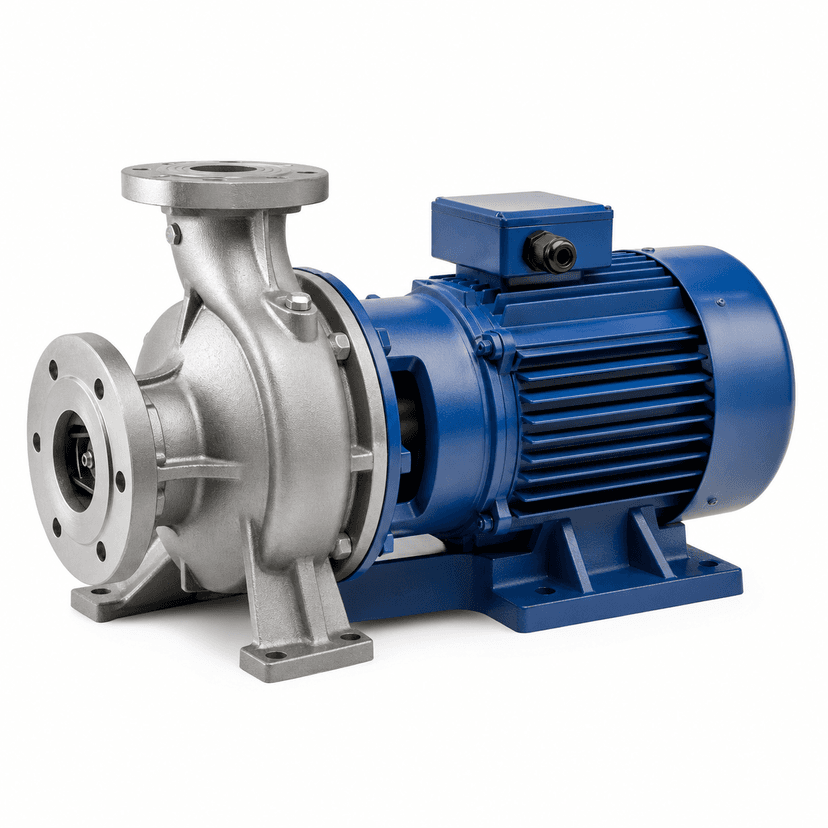
Investment-cast metallic centrifugal pumps with capacity up to 500 m3/hr and head up to 150 m for high-temperature chemical and industrial service.
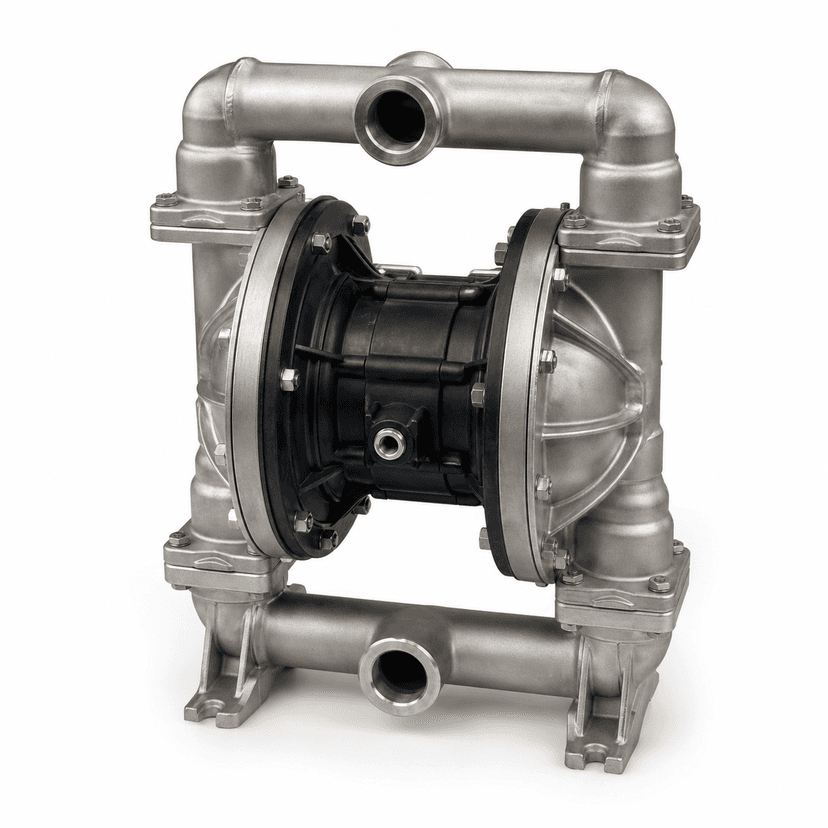
Pneumatic AODD pumps with no electric motor or seals, safe for hazardous areas, self-priming, and capable of running dry without damage.
Contact us for expert guidance on pump selection for your application.