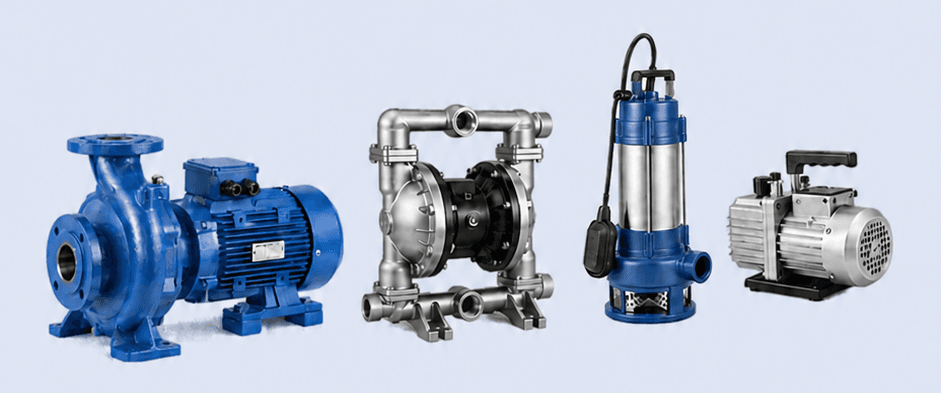
Corrosion-resistant pumps for acid, alkali, and solvent handling in chemical plants.
Industry Overview
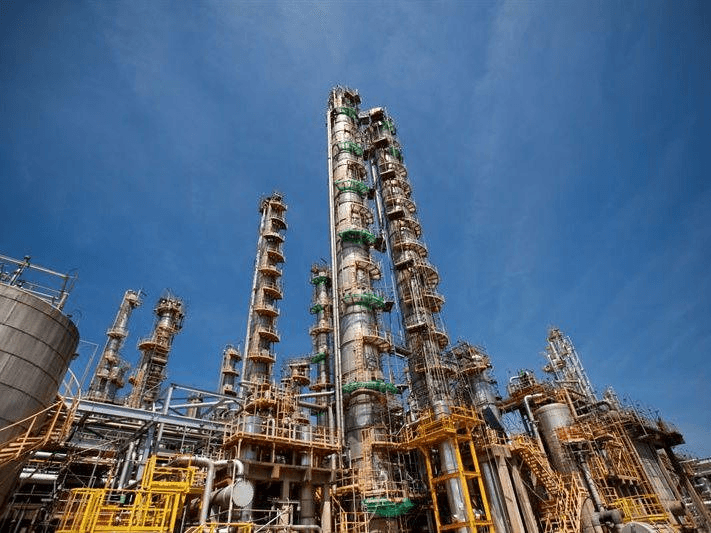
Chemical plants handle corrosive acids, alkalis, solvents, and reactive chemicals at varying temperatures and concentrations. Pumps in these environments need chemical-resistant wetted parts and reliable sealing to prevent hazardous leaks.
How We Help
Recommended Products
Suited for chemical industry applications.
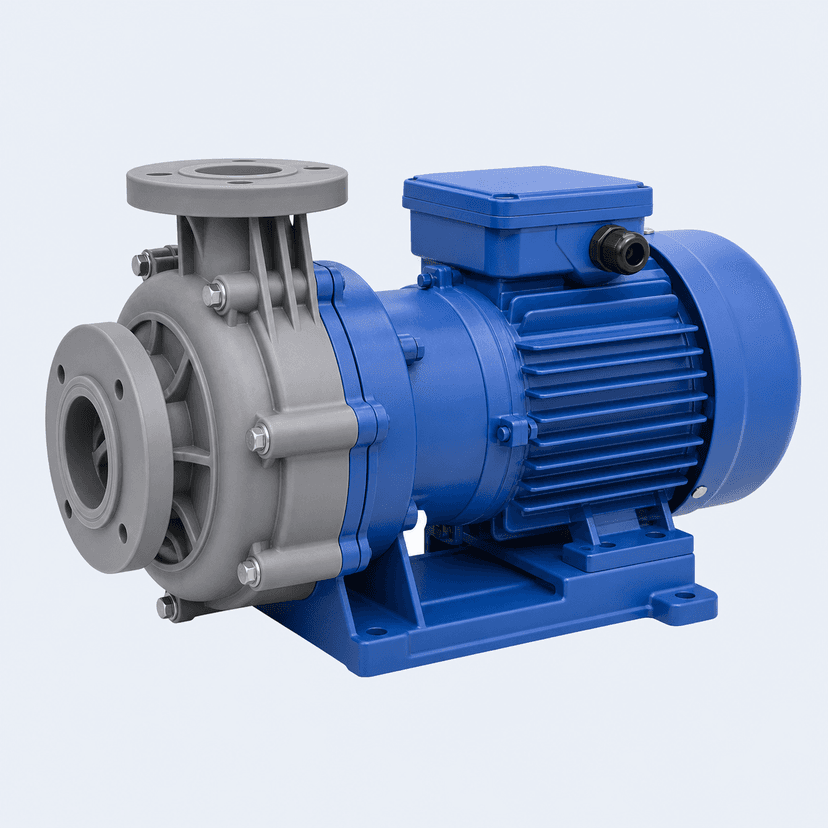
Horizontal centrifugal pumps with corrosion-resistant PP, PVDF, GRP, and UHMWPE construction for chemical and process industries.
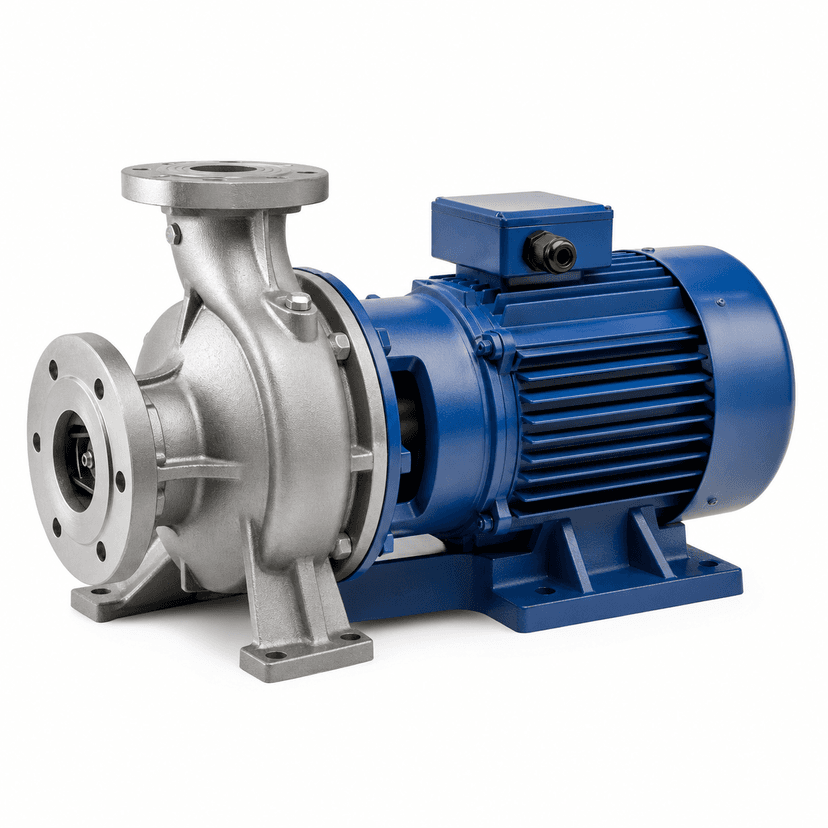
Investment-cast metallic centrifugal pumps with capacity up to 500 m3/hr and head up to 150 m for high-temperature chemical and industrial service.
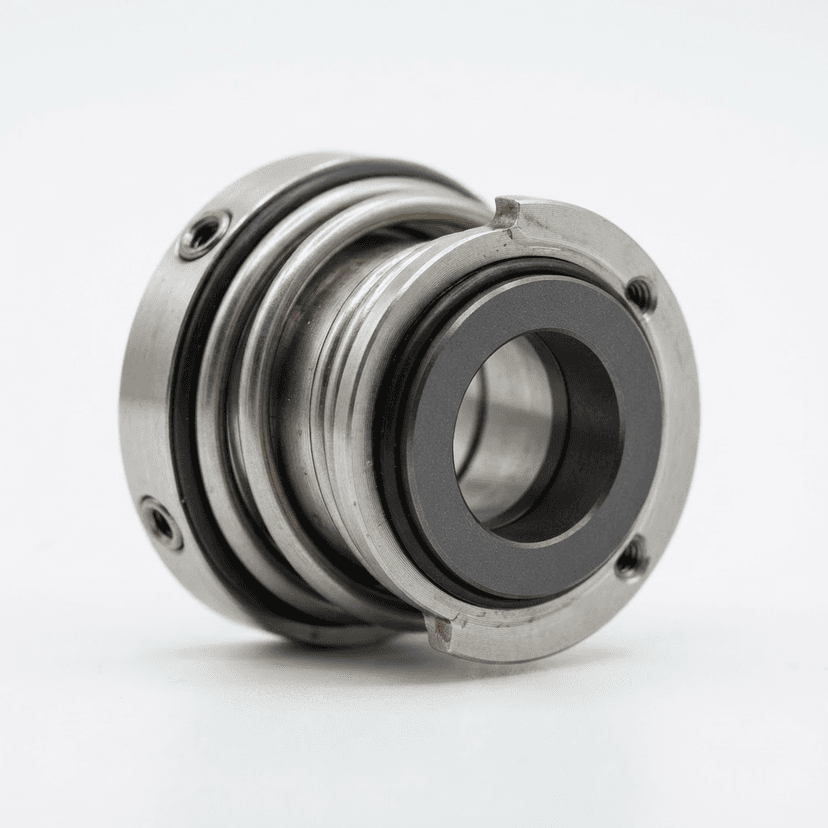
Six types of mechanical seals for pump shaft sealing in chemical, pharmaceutical, and process industry applications.
Let us help you choose the right pump for your specific process conditions.